Product Introduction
Types of UV Laser Marking Machines
-

FM-UD Laser Marking Machine
Rated 4.75 out of 5$5,070.00 – $12,090.00Price range: $5,070.00 through $12,090.00 Select options This product has multiple variants. The options may be chosen on the product page -
FM-UH Laser Marking Machine
Rated 4.50 out of 5$5,460.00 – $12,480.00Price range: $5,460.00 through $12,480.00 Select options This product has multiple variants. The options may be chosen on the product page -
FM-US Laser Marking Machine
Rated 4.75 out of 5$5,200.00 – $12,220.00Price range: $5,200.00 through $12,220.00 Select options This product has multiple variants. The options may be chosen on the product page -
FM-UP Laser Marking Machine
Rated 4.75 out of 5$5,330.00 – $12,350.00Price range: $5,330.00 through $12,350.00 Select options This product has multiple variants. The options may be chosen on the product page -
FM-UE Laser Marking Machine
Rated 4.88 out of 5$6,370.00 – $13,390.00Price range: $6,370.00 through $13,390.00 Select options This product has multiple variants. The options may be chosen on the product page -
FM-UF Laser Marking Machine
Rated 4.50 out of 5$7,150.00 – $14,170.00Price range: $7,150.00 through $14,170.00 Select options This product has multiple variants. The options may be chosen on the product page
Application of UV Laser Marking Machines
Why Choose Us
Precision Engineering
Our machines deliver ultra-fine marking and engraving with high-speed galvanometer systems and stable laser sources for consistent, reliable output.
Wide Material Compatibility
We offer different laser types to match your needs, ensuring crisp, permanent marks on metal, plastic, wood, leather, and more.
User-Friendly Software
Intuitive control software allows easy setup, flexible design import, and precise marking even for first-time users.
Customizable Solutions
We provide machine options tailored to your product size, line speed, and marking content for seamless integration.
Low Maintenance
Our systems run cleanly with no inks or chemicals, lowering long-term operating costs and environmental impact.
Dedicated Support and Service
Faster Laser offers professional training, remote troubleshooting, and responsive service to keep your production running smoothly.
UV Laser Marking Machines VS Other Marking Machines
| Feature / Machine Type | UV Laser Marking Machine | Dot Peen Marking Machine | Inkjet Printing Machine | Stamping Machine |
|---|---|---|---|---|
| Marking Method | Ultraviolet laser (cold marking) | Mechanical pin striking | Ink sprayed onto surface | Die pressed into material |
| Wavelength | 355 nm (short, high-precision beam) | Not applicable | Not applicable | Not applicable |
| Heat Impact | Very low (ideal for heat-sensitive materials) | None | None | High (due to force) |
| Marking Precision | Extremely high (micro-text, fine detail) | Moderate | Moderate | Low to moderate |
| Material Compatibility | Plastics, glass, ceramics, films, semiconductors | Mostly metals | Paper, cardboard, plastics | Metals and rigid materials |
| Suitable for Transparent Materials | Yes | No | No | No |
| Contact or Non-Contact | Non-contact | Contact-based | Non-contact | Contact-based |
| Marking Durability | Permanent, non-destructive | Permanent | Temporary (can smear or fade) | Permanent |
| Maintenance Requirements | Low (no consumables) | Moderate (mechanical parts) | High (ink and nozzle cleaning) | High (die wear and maintenance) |
| Environmental Impact | Minimal (no chemicals or ink) | Low | High (ink waste and VOCs) | Moderate |
| Setup Time | Short | Moderate | Short | Long (requires custom dies) |
| Operating Cost | Low (no ink or consumables) | Low | High (ink, solvents, maintenance) | Moderate (tooling and labor) |
| Noise Level | Low | High | Low | High |
| Automation Compatibility | Excellent (inline, robotic systems) | Limited | Good | Limited |
| Common Applications | Electronics, medical, plastics, glass, semiconductors | Metal parts, nameplates, tools | Packaging, date codes, labels | Coins, logos, heavy parts |
Customer Testimonials
Related Resources
What Are The Different Types Of Laser Marking Machines
This article provides an overview of laser marking machine types, covering fiber, CO2, UV, green, and ultrafast systems, as well as applications, features, selection factors, and practical applications in manufacturing.
Laser Marking VS Laser Engraving VS Laser Etching
This article explores laser marking, laser engraving, and laser etching, covering processes, materials, applications, quality control, costs, and selection criteria.
Laser Marking VS Pad Printing
This article explores the key differences between laser marking and pad printing, comparing their precision, durability, cost, material compatibility, and suitability for various applications.
Laser Marking VS Dot Peen Marking
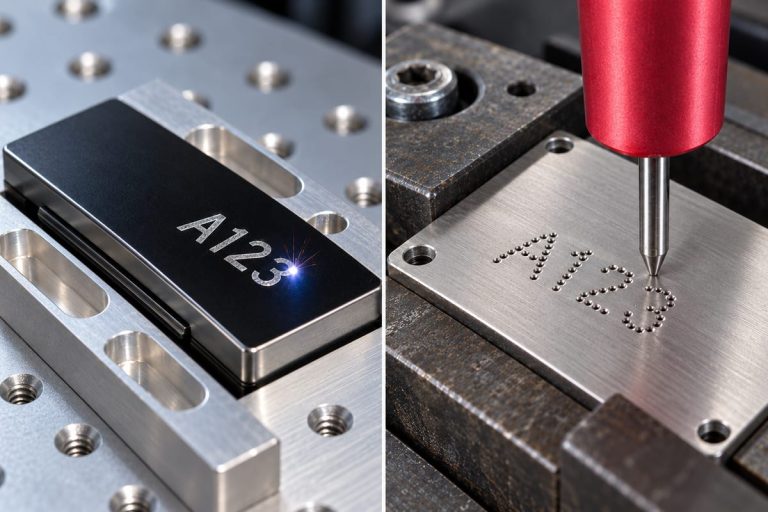
This article provides a comprehensive comparison of laser marking and dot matrix marking, explaining their principles, capabilities, applications, costs, and key factors for choosing the appropriate method.
Frequently Asked Questions
What Are UV Laser Marking Machines?
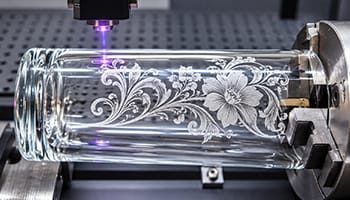
- Operating Principle: The pulsed UV laser directs energy through scanning and focusing optics to draw the programmed design. Depending on the material, the beam produces photochemical changes, surface discoloration, or controlled material removal. The process works without mechanical contact between a marking tool and the part.
- Reduced Thermal Impact: UV laser marking is often called “cold marking” because suitable processes can limit surrounding heat effects. This helps reduce charring, melting, or distortion on delicate parts. However, energy is still deposited in the material, and unsuitable settings can cause thermal damage.
- Material Compatibility: UV laser marking systems can mark many engineering plastics, transparent polymers, glass, selected ceramics, and metals. They are particularly useful when an infrared laser produces insufficient contrast or excessive damage. Exact compatibility depends on material composition, pigments, additives, coatings, and the required marking effect.
- Fine Detail and Small Codes: The short wavelength supports a small focused spot when combined with appropriate optics and beam quality. This enables fine lettering, narrow lines, and compact identification codes. Actual resolution also depends on focus, lens selection, positioning, and the material’s response.
- Marking Content and Durability: Typical output includes logos, serial numbers, production dates, barcodes, QR codes, and Data Matrix codes. Marks are formed directly on the material or its coating. Their resistance to abrasion, solvents, and repeated cleaning depends on the substrate and marking process.
- Industrial Applications: UV laser marking is used for electronic components, connectors, medical plastics, pharmaceutical packaging, and consumer products. Examples include identification on small resin housings, plastic bottles, glass components, and coated surfaces. Readability and product integrity should be validated for the intended manufacturing application.
- Equipment Configurations: Machines may be supplied as standalone workstations or integrated production-line systems. Depending on the model, options include autofocus, camera-based alignment, and three-dimensional focus control. These features help position designs and accommodate components with different shapes or surface heights.
- Practical Limitations and Safety: UV laser marking requires suitable operating parameters, clean optics, and the specified cooling arrangement. Conventional fiber lasers may be more productive for substantial metal engraving. Installations also need appropriate beam containment, laser safety controls, and material-specific fume extraction.
What Laser Power Options Are Available For UV Laser Marking Machines?
- 3W UV Lasers: Can be considered for small text, serial numbers, fine logos, and identification codes on compatible plastics and glass. This output can meet many light marking requirements when the material responds well. Larger filled designs may require longer processing times under otherwise comparable conditions.
- 5W UV Lasers: The widely offered configuration for electronic components, plastic housings, packaging, and consumer products. Additional average output can provide processing flexibility when moving beyond a lower-power system. Sample tests should confirm that the proposed settings achieve the required clarity, surface condition, and cycle time.
- 10W UV Lasers: Useful when production requires greater energy delivery for larger graphics, more extensive filled areas, or shorter marking cycles. Benefits depend on the source’s pulse characteristics and the material response. The actual improvement should be demonstrated using the intended artwork and production parts.
- 12W UV Lasers: The intermediate option between 10W and 15W. It can provide additional processing capacity where average output limits marking speed. Check the exact source model, because beam quality, pulse duration, and output at different repetition frequencies can differ between similarly rated products.
- 15W UV Lasers: The highest output among the five options listed, suitable for evaluation where demanding production workloads benefit from more available average power. Careful control of scanning speed, pulse frequency, and overlapping scan lines remains important to preserve surface quality and avoid excessive energy deposition.
- Average Power and Pulse Specifications: Average wattage provides only part of the comparison. Pulse energy, pulse duration, repetition frequency, beam quality, and output stability also affect results. Manufacturers often specify rated power at a particular frequency, so compare datasheets at the intended operating conditions.
- Precision and Material Response: Higher output does not automatically produce finer detail or better contrast. Resolution depends on the focused spot, optics, positioning, and material. UV laser marking can reduce thermal effects in suitable applications, but inappropriate settings can still cause discoloration, melting, or cracking.
- Cooling and Machine Configuration: UV laser sources may use air or water cooling, depending on their design. Confirm the specified cooling arrangement, environmental limits, scanner compatibility, and lens selection. Adequate extraction and stable focusing remain important across all five power levels.
What Are The Disadvantages Of UV Laser Marking Machines?
- Substantial Initial Investment: The UV laser source, compatible optics, scanning hardware, and safety equipment can make a complete system costly. Cameras, automatic focusing, and production integration increase the investment further. For simple, low-volume jobs, the additional expense may provide limited practical benefit.
- Lower Efficiency for Deep Metal Engraving: Many compact UV laser marking machines prioritize fine surface marking. Removing substantial amounts of metal or producing deep engravings may require repeated passes and extended processing time. Fiber lasers often provide greater productivity for these tasks, depending on the material and configuration.
- Material and Contrast Variability: Broad compatibility does not guarantee satisfactory results on every material. Polymer formulations, pigments, additives, coatings, and surface conditions affect absorption and contrast. The successful mark on one grade may require different parameters on another, increasing testing and process qualification work.
- Setup and Damage Risks: Power, pulse frequency, scanning speed, fill spacing, and focus need careful coordination. Although UV laser marking can reduce thermal effects, excessive energy or pulse overlap can still cause unwanted heating, ablation, or surface damage. “Cold marking” requires proper parameter development and validation.
- Optical Cleanliness and Specialized Maintenance: Contamination can reduce UV optical performance or contribute to damage. Clean optics, suitable extraction, and correct cleaning procedures are important. Internal faults involving the source or frequency-conversion components may require qualified servicing, replacement modules, and production downtime.
- Cooling and Environmental Requirements: Some UV laser sources require water cooling, adding chiller space, coolant checks, and temperature management. Air-cooled models still need adequate ventilation and clearance. The selected design’s environmental limits and servicing requirements must be included in installation planning and operating costs.
- Marking Field and Geometry Constraints: The fixed scanning field limits the area processed without repositioning. Fine marking also depends on maintaining the correct focus and stable part location. Curved surfaces or components with varying heights may require additional fixtures, rotary equipment, or three-dimensional focus control.
- Safety and Fume-Control Costs: Ultraviolet laser exposure can injure eyes and skin, so installations need suitable beam containment and safety controls. Material processing can also release airborne particles and gases. Appropriate extraction, protective equipment where required, operator training, and filter maintenance add ongoing responsibilities.
What Is The Price Of UV Laser Marking Machines?
- Laser Power: Available options include 3W, 5W, 10W, 12W, and 15W. Higher output generally increases the source cost and may provide additional production capacity. Select power according to the tested material response and required cycle time; wattage alone does not determine precision or marking quality.
- Laser Source Specifications: Sources with identical wattage can differ in pulse duration, repetition frequency, pulse energy, beam quality, and output stability. These characteristics affect processing capability and quotation value. Ask for the exact manufacturer, source model, technical specifications, and warranty coverage when comparing machines.
- Cooling Equipment: UV laser marking systems may use air cooling or water cooling, depending on their design. For a water-cooled configuration, confirm whether a correctly sized chiller, connecting hoses, and required accessories are included. Consider installation space, electricity, coolant maintenance, and environmental requirements when calculating ownership costs.
- Marking Area and Optics: The field lens, scanning head, working distance, and focusing features influence the machine’s capabilities and price. Additional lenses or three-dimensional focus control can increase costs. Compare quotations using the same marking field and demonstrated ability to produce the required detail.
- Machine Construction and Enclosure: The basic split system and a fully enclosed workstation contain different structural and safety components. Interlocked doors, suitable viewing windows, motorized height adjustment, and ergonomic loading features add equipment costs. Check the supplied configuration and the parts needed for the intended installation.
- Software and Automation: Confirm the included marking software, license conditions, controller compatibility, and update policy. Camera alignment, autofocus, automatic positioning, and production-line interfaces may involve additional charges. Establish whether variable data, code generation, and other required functions are included in the quoted package.
- Extraction and Accessories: Fume extractors, ducting, rotary devices, custom fixtures, and a control computer may be included or supplied separately. Choose extraction according to the actual materials and coatings. Request an itemized equipment list so the complete installation can be compared across suppliers.
- Delivery, Training, and Support: Freight, insurance, taxes, import duties, installation, and operator training affect the total delivered cost. Warranty terms, repair arrangements, spare-parts availability, and local service also matter. Confirm which components, labor, and transport expenses are covered if a fault occurs.
What Materials Can Be Marked With UV Lasers?
- Engineering Plastics: Selected grades of ABS, polycarbonate, polyamide, PBT, PEEK, polyethylene, and polypropylene can receive clear identification marks. Applications include molded housings, connectors, bottles, and medical components. Pigments, fillers, and additives influence whether the mark becomes darker, lighter, or insufficiently visible.
- Thin Films and Flexible Packaging: Suitable polymer films, multilayer pouches, and blister-pack materials can be marked with dates, batch numbers, and codes. The process must be matched to the layer structure and thickness so the required contrast is achieved while preserving package integrity.
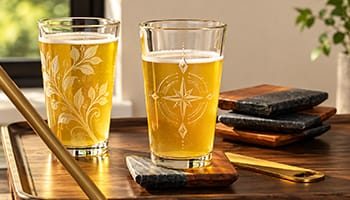
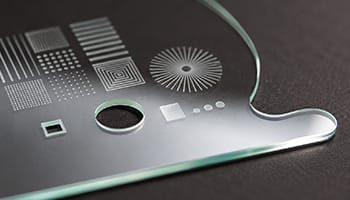
- Glass and Quartz: UV lasers can create fine surface marks on suitable glass bottles, instrument glass, and selected quartz components. Typical uses include logos, traceability codes, and measurement scales. Glass composition and processing conditions affect visibility, surface texture, and the risk of cracking.
- Ceramics: Compatible technical ceramics, electronic ceramic packages, and selected glazed surfaces can receive small identification marks and decorative details. Results vary with composition, glaze, surface finish, and absorption. Verify mark contrast and check that the finished surface meets its mechanical and functional requirements.
- Rubber and Elastomers: Selected rubber compounds and flexible polymers can be marked for seals, buttons, and other molded parts. UV laser marking processing can help control the surface effect, but fillers and formulation strongly influence contrast. The laser marking should preserve the flexibility and function needed by the component.
- Metals: Suitable UV laser marking systems can mark stainless steel, aluminum, copper, brass, and selected precious metals. Results depend on the alloy, finish, and intended marking effect. For substantial metal removal or deep engraving, a fiber laser may provide better productivity than compact UV laser marking machines.
- Painted, Coated, and Anodized Surfaces: UV lasers can modify or selectively remove compatible surface layers to create contrasting text and graphics. Examples include coated components and anodized aluminum labels. Check whether the finished mark preserves any required corrosion protection or other coating function.
- Silicon and Electronic Materials: Silicon surfaces, selected semiconductor packaging resins, and suitable PCB substrates can receive fine identification marks. These applications require controlled processing depth and positioning. Qualification should confirm that marking does not compromise sensitive structures, conductive features, or the component’s intended performance.
- Paper and Cardboard: Selected paper grades, coated cartons, and packaging boards can receive production codes and branding. Coatings, pigments, and printing layers influence the achievable contrast. Settings must suit the material thickness and finish to control unwanted discoloration or surface damage.
What File Formats Do UV Laser Marking Machines Support?
- DXF Files: DXF is commonly used for CAD geometry, technical symbols, and accurately sized outlines. It is suitable for designs that need controlled dimensions and clear paths. After importing, verify units, scale, curve quality, and duplicate lines before applying outline or hatch marking settings.
- AI Files: Adobe Illustrator artwork is useful for logos, lettering, and vector illustrations. Supported Illustrator versions and design features differ between marking programs. Convert text to outlines when necessary, simplify unsupported effects, and inspect the imported artwork to preserve the intended appearance.
- SVG Files: SVG provides scalable vector graphics for symbols, logos, and detailed layouts. LightBurn supports SVG, and selected EZCAD versions also list it. Confirm compatibility with the installed software, especially for files containing clipping masks, gradients, embedded images, or other complex features.
- PLT and HPGL Files: These plotter formats transfer line paths and curves from compatible design programs. EZCAD lists PLT support, while LightBurn accepts PLT and HPGL. They can be useful for straightforward vector artwork, although fills and text should be checked after conversion.
- Bitmap Image Files: BMP, JPG/JPEG, PNG, GIF, and TIF/TIFF are supported by common marking programs. These formats suit photographs, shaded graphics, and raster logos. Source resolution, image contrast, grayscale conversion, and dithering affect the final result. JPEG compression artifacts may become visible in small details.
- PDF and CorelDRAW Workflows: PDF artwork can be imported into LightBurn, while other marking applications may require conversion. When direct CDR import is unavailable, export CorelDRAW designs to a supported format such as DXF, SVG, or AI. Verify the resulting dimensions, fonts, and graphic elements.
- CSV and TXT Production Data: Compatible software can use external data to populate names, serial numbers, part references, and batch information. LightBurn offers CSV merging, while EZCAD supports TXT and other variable-text sources. These files provide content for a prepared marking layout rather than importing complete artwork.
- Native Project Files: Programs also save editable jobs in their own formats, such as EZD for EZCAD2 and LBRN2 or LBRN for LightBurn. These files retain layouts and job settings for reuse. Check software compatibility and the selected machine configuration when reopening an existing project.
What Are The Cooling Methods For UV Laser Marking Machines?
- Air Cooling: Air-cooled laser sources transfer heat into heat sinks or other cooling surfaces, with airflow carrying it away. Fans may assist this process. The arrangement avoids an external water circuit and can simplify installation. Commercial air-cooled UV laser marking machine designs include 3W and 5W models.
- Water Cooling: Water-cooled laser sources circulate an approved coolant through cooling passages or a cooling plate connected to the laser. The pump typically moves coolant through a chiller, where heat is removed before the liquid returns. Water-cooled designs include some 3W and 5W sources, illustrating the importance of checking the exact model.
- Heat Conduction Inside the Source: Internal components transfer heat through their mounts and heat-spreading structures toward the cooling interface. Some UV laser sources combine conduction with air convection. Conduction therefore forms part of the source’s overall cooling design and helps move heat away from sensitive components.
- Temperature Regulation: The temperature-controlled cooling system maintains the conditions specified for stable laser operation. For water-cooled machines, the chiller regulates coolant temperature around its approved setpoint. Follow the source manufacturer’s temperature and stability requirements, since unsuitable settings can affect performance or reliability.
- Chiller Selection: Choose a chiller using the specified cooling capacity, flow rate, pressure limits, and temperature stability. Laser output wattage alone is insufficient for sizing because the equipment generates additional waste heat. Confirm the required capacity at the expected room temperature and production duty.
- Cabinet and Chiller Ventilation: Controllers, power supplies, and other cabinet components may also use fans. The air-cooled water chiller releases collected heat into the surrounding air. Provide the recommended clearance and room ventilation so hot exhaust does not circulate back into cooling intakes.
- Coolant and Condensation Control: Use the water quality or prepared coolant approved for the source and chiller. Monitor room temperature and humidity to manage condensation risk. Keep coolant settings within approved limits and control humidity so cooled surfaces exposed to room air remain above the dew point.
- Maintenance and Protective Alarms: Inspect airflow paths, fans, coolant levels, hoses, and filters according to the maintenance schedule. Address leaks, restricted circulation, and temperature alarms promptly. Flow and temperature protection should remain functional so the machine can respond correctly to a cooling fault.
How To Maintain UV Laser Marking Machines?
- Safe Shutdown and Preparation: Follow the specified shutdown and cooldown sequence before maintenance. Disable laser emission and isolate electrical power before cleaning or mechanical work, using the required lockout procedure. Restrict each task to trained personnel and restore guards before returning the machine to operation.
- Optical Inspection and Cleaning: Inspect accessible protective windows and lens surfaces for dust, deposits, or damage. Clean contaminated surfaces using approved optical wipes and cleaning fluid, following the manufacturer’s method. Handle coatings carefully, since scratches or residues can reduce marking quality and damage UV laser optics.
- Air-Cooling Maintenance: Keep ventilation openings, heat sinks, fans, and cabinet filters clear. Clean or replace accessible filters according to the manual and their condition. Maintain the specified equipment clearance, and investigate unusual fan noise, restricted airflow, or rising operating temperatures.
- Water-Cooling Maintenance: Where a chiller is fitted, check coolant level, condition, temperature, circulation, and hose connections. Use the coolant approved for both the source and chiller. Replace coolant and service filters at the specified intervals, and address leaks, contamination, or flow alarms promptly.
- Fume-Extraction Maintenance: Check that capture nozzles and hoses remain correctly positioned and unobstructed. Monitor airflow and filter indications, and replace particulate and gas filters according to manufacturer guidance and process conditions. Gas filters can become exhausted before a pressure alarm appears. Use appropriate handling and disposal procedures for contaminated filters and residues.
- Worktable, Fixtures, and Motion Components: Remove processing debris from the work area and fixtures using suitable methods. Inspect clamps, rotary attachments, and positioning mechanisms for looseness or wear. Lubricate only the components and locations specified by the manufacturer, and confirm repeatable part positioning afterward.
- Electrical and Safety Checks: Visually inspect accessible cables, connectors, and grounding connections for damage. Check emergency stops, enclosure interlocks, indicators, and other safety functions using approved test procedures. Electrical faults and damaged safety components should be assessed and repaired by qualified personnel before production resumes.
- Software Backups and Performance Checks: Back up validated marking jobs, machine settings, and calibration files. Run a reference marking test under normal safety controls and compare focus, position, contrast, dimensions, and code readability with recorded results. Investigate unexpected changes before accepting production output.
- Records and Specialist Service: Record inspections, cleaning, coolant changes, filter replacements, alarms, and repairs. Arrange qualified servicing for internal laser faults, optical alignment, calibration, or electrical work beyond the operator’s authorized scope. Keep service contacts and replacement-part information available.