Product Introduction
Types of Tube Laser Cutting Machines
-

FT-C Laser Cutting Machine
Rated 4.38 out of 5$29,250.00 – $218,400.00Price range: $29,250.00 through $218,400.00 Select options This product has multiple variants. The options may be chosen on the product page -
FT Laser Cutting Machine
Rated 4.75 out of 5$35,750.00 – $224,900.00Price range: $35,750.00 through $224,900.00 Select options This product has multiple variants. The options may be chosen on the product page -
FT-A Laser Cutting Machine
Rated 5.00 out of 5$94,250.00 – $283,400.00Price range: $94,250.00 through $283,400.00 Select options This product has multiple variants. The options may be chosen on the product page
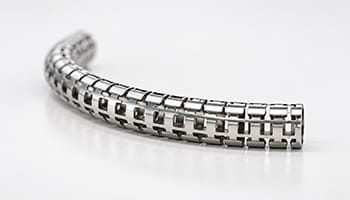
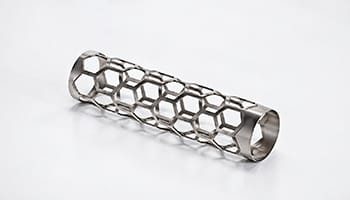
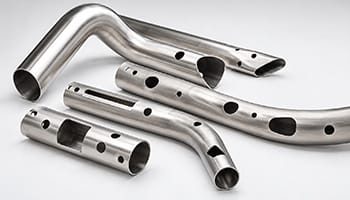
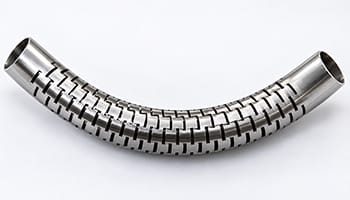
Application of Tube Laser Cutting Machines
Why Choose Us
Cutting-Edge Technology
Every Faster Laser machine is built with the latest advancements, ensuring precise cuts, faster operation speeds, and the ability to handle complex designs effortlessly.
Superior Build Quality
We use only premium-grade materials and components, ensuring that every machine delivers consistent performance and maintains durability under heavy use.
Customized Solutions
Our team works closely with each customer to develop tailored laser cutting solutions that meet specific production needs and business objectives.
Comprehensive Support
Faster Laser provides thorough training, responsive technical support, and ongoing maintenance services to keep your machines running at peak efficiency.
Cost-Effective Investment
We offer high-quality laser cutting machines at competitive prices, ensuring you get maximum performance and long-term value from your investment.
Proven Industry Experience
With years of expertise and a strong global client base, Faster Laser has built a reputation for reliability, innovation, and customer satisfaction.
Tube Laser Cutting Machines VS Other Cutting Machines
| Comparison Item | Tube Laser Cutting Machine | Plasma Cutting Machine | Waterjet Cutting Machine | Flame Cutting Machine |
|---|---|---|---|---|
| Cutting Method | Fiber laser beam | Ionized gas arc | High-pressure water with abrasive | Oxy-fuel combustion |
| Tube Cutting Capability | Built-in rotary system for all tube shapes | Not designed for tubes (manual setup needed) | Limited, requires complex fixtures | Not suitable for round or shaped tubes |
| Cutting Precision | Very high | Moderate | High | Low |
| Edge Quality | Clean, smooth, burr-free | Rough, often needs finishing | Smooth, minimal burring | Rough and oxidized |
| Cutting Speed | Fast | Fast | Slow to moderate | Slow |
| Hole and Slot Cutting | Precise and consistent | Inconsistent on round surfaces | Possible but slow | Difficult and inaccurate |
| Bevel and Angle Cutting | Automated, accurate | Possible but limited | Difficult and time-consuming | Very limited |
| Material Compatibility | Metals: SS, CS, aluminum, brass, copper | Conductive metals only | Most materials | Carbon steel only |
| Heat Affected Zone (HAZ) | Very small | Medium | None | Large |
| Automation & CNC Integration | Excellent | Good | Limited | Poor |
| Repeatability | High | Moderate | High | Low |
| Maintenance Requirements | Low | Moderate | High | Low |
| Operating Cost | Low | Moderate | High (abrasives, water use) | Low |
| Setup Time | Fast, automated | Manual alignment required | Long setup time | Manual and slow |
| Typical Industry Applications | Fitness, auto parts, furniture, structures | General metal cutting | Aerospace, prototyping | Heavy industrial, structural steel |
Customer Testimonials
Related Resources
What Is The Cost Of Laser Cutting Machines?
This article explores laser cutting machine price ranges, installation and operating costs, financing, ROI, and the key factors that determine total cost of ownership for buyers.
What Should You Consider Before Buying Laser Cutting Machines
This article is a comprehensive guide on what to consider before buying laser cutting machines, covering production requirements, laser technology, machine configuration, operating costs, vendor support, and testing.
Does Laser Cutting Require Assist Gases
This article explains whether assist gas is required for laser cutting, covering how it works, when it’s necessary, gas types, quality impact, costs, safety factors, and practical decision guidance.
Laser Cutting VS Flame Cutting
This article compares laser cutting and flame cutting, exploring their differences in precision, material versatility, speed, cost, and applications to help industries choose the right cutting method.
Frequently Asked Questions
What Are Tube Laser Cutting Machines?
- Working Principle: The fiber laser source generates the beam, which travels through an optical delivery fiber to the cutting head. Focusing optics concentrate energy onto the tube wall, melting the metal. Assist gas clears molten material from the cut while controlled motion produces the required geometry.
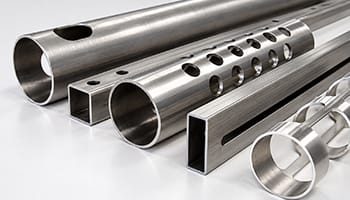
- Tube Shapes and Materials: These machines commonly process round, square, rectangular, and oval tubing. Some configurations also handle special profiles and open sections. Typical materials include carbon steel, stainless steel, and aluminum; appropriately equipped systems can also cut copper, brass, galvanized steel, and selected alloys.
- Main Components: The typical machine includes the laser source, cutting head, rotary chucks, feeding mechanism, support devices, CNC controller, cooling equipment, gas supply, and extraction system. Chucks grip and position the tube, while suitable supports help control sagging and vibration during feeding, rotation, and cutting.
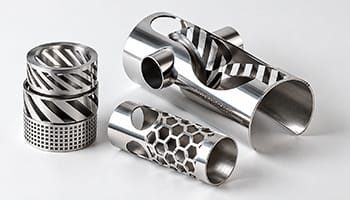
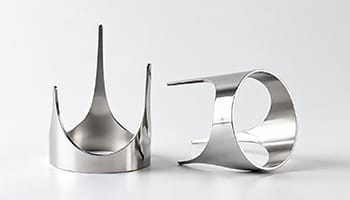
- Cutting Operations: Tube lasers can cut parts to length and produce holes, slots, notches, angled ends, and intersecting joint profiles. Machines equipped with suitable tilting or 3D cutting heads can also produce bevels. These features help prepare components for fitting, welding, and assembly.
- CNC Programming and Nesting: CAD/CAM software converts digital tube designs into coordinated cutting programs. Tube nesting arranges parts along the available stock length to improve material utilization. Programming also considers cutting sequences, joint geometry, support positions, and machine limitations, helping maintain consistency across repeated production batches.
- Loading and Automation: Systems are available with manual, assisted, or automatic material handling. Bundle loaders, automatic supports, and controlled unloading can reduce handling work and support continuous production. Features for reducing uncut tail material depend on chuck arrangement, part design, and the specific machine configuration.
- Capacity and Cutting Quality: Machine suitability depends on tube diameter or profile dimensions, wall thickness, stock length, weight, and required finished-part length. Diameter and wall thickness are separate limits. Accuracy and edge quality also depend on tube straightness, clamping, material condition, laser power, and processing parameters.
- Industrial Applications: Tube laser cutting is used for metal furniture, fitness equipment, vehicle components, machinery frames, railings, agricultural equipment, and structural assemblies. Its programmable workflow supports prototypes, customized components, and repeated batches, especially when several cutting features are needed on the same tubular part.
How Do Tube Laser Cutting Machines Work?
- Design and Programming: CAD/CAM software converts the component drawing into cutting instructions. The program defines holes, slots, end profiles, cutting sequences, and processing parameters. Nesting arranges several parts along the stock length while accounting for cutting gaps, clamping requirements, and remaining material.
- Tube Loading and Clamping: Operators or automatic loaders place the tube into the machine. Rotary chucks grip and position it, while support devices help control sagging and vibration. Suitable clamping pressure holds the workpiece securely without unnecessarily deforming thin walls. Tube dimensions and material must match the program.
- Laser Generation and Delivery: Pump diodes supply energy to a specially doped optical fiber inside the laser source, generating the cutting beam. The delivery fiber carries that beam to the cutting head, where optical components prepare it for precise focusing onto the workpiece.
- Focusing and Surface Tracking: The cutting head concentrates the beam into a small spot, creating sufficient energy density to melt metal locally. Height sensing and controlled head movement help maintain nozzle clearance as the tube moves. Focus settings are selected for the material, wall thickness, and cutting process.
- Piercing the Tube Wall: For features starting within the wall, the laser first creates an opening through the material. Piercing settings control how energy and gas are applied before contour cutting begins. Some machines monitor breakthrough to improve consistency and reduce unnecessary piercing time or spatter.
- Assist-Gas Cutting: Gas flows through the nozzle alongside the beam and expels molten metal from the narrow cut. Oxygen can support an additional heat-producing reaction when cutting carbon steel. Nitrogen helps limit edge oxidation, while suitably treated compressed air is used for selected applications.
- Coordinated Motion and Feature Cutting: The controller synchronizes tube feeding, chuck rotation, head position, and laser output to follow the programmed geometry. This produces straight cuts, holes, notches, and intersecting end profiles. Machines with suitable tilting heads can also create bevels for subsequent fitting or welding.
- Part Separation and Inspection: The machine separates completed components according to the programmed sequence. Supported unloading systems or trained operators collect parts under safe conditions. Inspection checks length, feature positions, edge quality, and internal spatter where relevant. Some components require deburring or cleaning before assembly.
What Is The Price Of Tube Laser Cutting Machines?
- Laser Power and Source Configuration: Higher laser power generally increases equipment cost and can expand cutting capability or improve processing speed. Source brand, specifications, warranty, and service support also influence pricing. Match the source to material, wall thickness, and required output, using representative cutting trials to confirm performance.
- Tube Size, Length, and Weight Capacity: Machines designed for larger profiles, longer stock, or heavier tubes require appropriate beds, chucks, drives, and support systems. These requirements influence the price. Compare maximum round-tube diameter, square or rectangular profile capacity, loading length, finished-part length, and allowable tube weight separately.
- Chuck and Support Design: Machines with two, three, or four chucks offer different handling and workholding capabilities. Synchronized chucks and following supports can improve control of long or heavy components and reduce unusable tail material on suitable jobs. Evaluate the complete mechanism, including gripping range and support capacity.
- Loading and Unloading Automation: Manual loading, assisted feeding, bundle loaders, and automatic unloading create different purchase costs and labor requirements. Automated handling can support continuous production, but compatibility depends on tube shape, dimensions, weight, and batch size. Confirm exactly which loading and collection equipment is included.
- Cutting Head and Bevel Options: Autofocus capability, monitoring features, power rating, and optical protection affect cutting-head specifications and cost. The suitable tilting or 3D head adds bevel-cutting capability. Determine whether angled weld preparation is required and confirm that the quoted machine includes the necessary hardware and software.
- Controls and Advanced Functions: Tube nesting, cutting simulation, weld-seam recognition, profile measurement, and production-management connections can influence configuration and pricing. Some functions are optional or separately licensed. Ask which software modules, file interfaces, updates, and technical assistance are covered by the quotation.
- Supporting Equipment: Chillers, extraction systems, required guarding, gas regulators, and related accessories contribute to the complete project budget. Compressed-air cutting may require a suitable compressor, dryer, and filtration system. Check which auxiliary equipment comes with the machine and which must be purchased separately.
- Delivery, Installation, and Service: Freight, insurance, duties, taxes, unloading, commissioning, training, and site preparation may add to the quoted equipment price. Compare offers using the same delivery terms. Review warranty coverage for the source, head, controls, and mechanical systems, including service labor and technician travel.
- Ongoing Operating Costs: Electricity, assist gas, consumables, lubrication, maintenance, and labor continue throughout production. Scrap and downtime also affect the cost per accepted part. The lower purchase price can lose its advantage if the machine processes the required work slowly or lacks dependable support.
What Is The Maximum Tube Diameter That Tube Laser Cutting Machines Can Cut?
- Outside Diameter Measurement: For round tubes, capacity refers to the external diameter measured across the tube. Internal bore size and nominal pipe designations can differ from this measurement. Confirm the actual outside diameter, including permitted manufacturing variation, against the machine’s approved processing range.
- Chuck Opening and Gripping Range: Verify both the 20 mm minimum and 500 mm maximum against the fitted jaws and approved clamping range. Jaw travel, gripping engagement, and through-chuck clearance must suit the intended stock. Some configurations require different tooling to hold smaller tubes securely.
- Square and Rectangular Profiles: Round-tube diameter ratings do not establish the allowable dimensions of other sections. Check square side lengths, rectangular dimensions, and rotational clearance separately. The outermost corners affect the space required during rotation, so obtain the manufacturer’s approved limits for each profile shape.
- Wall Thickness and Laser Power: Outside diameter and wall thickness are separate specifications. The laser source, cutting head, assist gas, and material properties determine wall-cutting capability. The tube that fits the chucks must also fall within the validated thickness range for its alloy and required edge quality.
- Tube Length and Weight: Check the complete tube weight and any specified weight-per-length limit at the intended stock length. The large-diameter, thick-walled tube can place substantial loads on the machine. Rated diameter, maximum length, and maximum weight should be checked together for the proposed workpiece.
- Support and Clamping Stability: Long or flexible tubes need suitable supports to control sagging and vibration. Following rollers and synchronized chucks help maintain alignment during feeding and rotation. Clamping must provide secure positioning while avoiding damage to thin walls, particularly when processing stock near the machine’s limits.
- Loading and Unloading Compatibility: Confirm that loaders, feeding racks, transfer mechanisms, and unloading supports accommodate the required tube dimensions and weight. Automatic handling equipment may have its own operating range. Check the complete workflow, including the length and weight of finished components, rather than only the cutting station.
- Cutting-Head Access and Verification: Bevels, complex end profiles, and features close to the chucks require suitable head access and collision clearance. Review the actual component drawings with the supplier. Simulation and sample cutting help establish whether the proposed diameter can be processed accurately at the required production rate.
What Shapes Of Tubes Can Tube Laser Cutting Machines Cut?
- Round Tubes: Circular tubes are among the most common options. CNC-controlled chucks rotate and feed the stock so the laser can produce holes, slots, notches, and joint profiles around the circumference. Suitability depends on outside diameter, wall thickness, and the machine’s approved processing range.
- Square Tubes: Square hollow sections have equal width and height, usually with rounded corners. Fiber lasers can cut features across their faces and ends for frames and assemblies. Programming must account for actual corner geometry, while secure clamping maintains consistent positioning during rotation.
- Rectangular Tubes: Rectangular hollow sections have different width and height dimensions. They can be cut to length and processed with mounting holes, slots, notches, and end profiles. Check both side dimensions and rotational clearance, since a round-tube diameter rating does not automatically establish rectangular capacity.
- Oval and Elliptical Tubes: These curved sections can be processed on suitably configured machines. Correct orientation and centering are important because their major and minor dimensions differ. The cutting program and head movement must follow the actual cross-section while maintaining appropriate nozzle clearance.
- Obround Tubes: Often described as racetrack-shaped sections, obround tubes have parallel straight sides joined by curved ends. Suitable machines can produce features along both areas. Workholding and programming must accommodate the transitions between flat and curved surfaces without losing alignment or cutting consistency.
- D-Shaped Tubes: These sections combine a flat side with a curved side. They can be processed when the jaws, centering method, and software support the geometry. Maintaining a repeatable angular orientation helps place cutouts correctly relative to the flat face and other assembly features.
- Polygonal Tubes: Triangular, hexagonal, trapezoidal, and other polygonal hollow sections are supported by selected machines. Their corners and changing face orientations require suitable cutting paths and clearance checks. Confirm the complete cross-section, including corner radii and dimensional variation, before approving production.
- Custom and Special Sections: Some machines process teardrop, concave, asymmetric, or other purpose-designed profiles. These may require dedicated jaws, additional centering functions, and specialized software. Submit detailed drawings and representative stock so the supplier can verify gripping, support, head access, and cutting performance.
- Open Structural Profiles: Compatible tube laser cutting machines can also process angles, channels, and selected I and H sections. Their open cross-sections require appropriate handling, workholding, and toolpath planning. This capability should be confirmed for the particular machine, profile dimensions, and required features.
How To Maintain Tube Laser Cutting Machines?
- Safe Shutdown: Before physical cleaning or servicing, follow the manufacturer’s shutdown and lockout procedures. Secure tubes and moving assemblies, isolate energy sources, and control stored pneumatic pressure. Allow hot components to cool. Electrical repairs and internal laser servicing require qualified personnel.
- Cutting Head and Optics: Inspect protective windows, nozzles, and ceramic components for contamination or damage. Clean accessible optics only with approved materials and procedures in a clean environment. Replace damaged consumables promptly, and avoid touching optical surfaces. Leave internal optical servicing to authorized technicians.
- Chucks and Clamping Jaws: Remove chips and dust from chuck jaws after each shift. Inspect jaw wear, gripping security, pneumatic connections, and rotation. Lubricate designated points as specified. Stop operation if tubes slip, chucks make abnormal noises, or their rotation becomes unsynchronized.
- Tube Supports and Feeders: Clear debris from support rollers, loading racks, and feeding mechanisms. Check for worn rollers, loose fasteners, and misaligned supports. Proper support helps prevent long tubes from sagging or vibrating during rotation.
- Motion System Lubrication: Clean guide rails, racks, and other specified transmission components. Apply the recommended lubricant in the correct quantity and at the prescribed intervals. Check automatic lubrication reservoirs and delivery lines where fitted.
- Cooling System: Check coolant level, temperature, circulation, and hose condition. Clean chiller filters and heat exchangers according to the manual. Use only approved coolant, replace it at specified intervals, and follow the manufacturer’s precautions against overheating, condensation, and freezing.
- Assist Gas System: Inspect hoses, regulators, connections, filters, and dryers. Maintain the specified gas purity and pressure, and investigate leaks using approved methods. Keep compressed air dry and free from oil contamination to protect optics and cutting quality.
- Fume Extraction and Waste Removal: Remove accumulated slag and scrap, maintain extraction airflow, and service dust collector filters as instructed. Use cleaning methods suitable for the collected metal dust, avoiding practices that disperse it throughout the workshop.
- Accuracy and Safety Checks: Follow prescribed procedures for nozzle centering, height calibration, and chuck alignment, particularly after collisions or component replacement. Check guards, interlocks, and emergency stops without bypassing them. Verify cutting quality with a sample part before restarting production.
How Do Tube Laser Cutting Machines Reduce Material Waste?
- Optimized Tube Nesting: CAD/CAM software arranges required part lengths and compatible end profiles along the tube. Mixing suitable short and long components within a production batch can fill otherwise unused lengths. Nesting must account for kerf, clamping zones, trimming, and unloading requirements.
- Narrow Cutting Kerf: The focused fiber laser removes a narrow strip of metal along each cutting path, limiting material lost during separation. Kerf compensation helps maintain finished dimensions, although actual kerf width varies with tube material, wall thickness, optics, and cutting parameters.
- Common-Line Cutting: Where part geometry and software allow, adjacent components can share one separating cut. This reduces extra gaps and duplicate cutting between parts. Compatible straight or complementary ends offer useful opportunities, provided dimensional tolerances, cut quality, and part stability remain acceptable.
- Reduced End Scrap: Suitable chuck arrangements and supported tube transfers allow some machines to cut closer to the tube’s end. This reduces the length left unprocessed for gripping. Minimum tail length depends on machine configuration, tube geometry, and the final part’s features.
- Remnant Reuse: Usable offcuts can be identified, measured, and allocated to later jobs with matching material specifications. Recording their grade, profile, wall thickness, and length helps prevent reusable stock from being discarded. Each remnant must meet the machine’s minimum loading and clamping requirements.
- Fewer Rejected Parts: CNC positioning and consistent tube support help keep holes, slots, and end profiles within specification. Machines equipped with appropriate sensing can compensate for certain stock variations or monitor cutting conditions. Correct settings and maintenance also help reduce avoidable scrap.
- Integrated Processing: Cutting to length, making holes, and producing complex end profiles in one setup reduces repeated positioning and handling. This can prevent errors that would otherwise spoil partially finished tubes and can reduce extra material allowances needed for subsequent operations.
- Better Stock Length Planning: Production software can compare available tube lengths against order quantities to identify combinations that leave less scrap. Purchasing suitable stock lengths and grouping compatible orders improves yield, especially when a fixed stock length poorly matches the required parts.
How Do Tube Laser Cutting Machines Reduce The Risk of Tube Deformation?
- Noncontact Cutting: The laser beam cuts without a physical cutting tool pushing against the tube wall. This avoids the tool forces associated with operations such as punching or sawing, reducing the chance of bending, denting, or collapsing delicate sections during material removal.
- Localized Heat Input: The tightly focused fiber laser concentrates energy along a narrow cutting path. Suitable cutting speeds limit heating time and help restrict the heat-affected zone. Less widespread heating reduces uneven thermal expansion and contraction, although thermal distortion remains possible.
- Optimized Cutting Parameters: Matching power, speed, focus, piercing, and assist gas to the material and wall thickness avoids unnecessary heat accumulation. Excessive pauses, repeated piercing, or poorly chosen settings can overheat thin walls, so validated cutting recipes are more useful than simply maximizing speed.
- Controlled Clamping Force: Correctly matched jaws hold the tube securely without excessive squeezing. Machines with adjustable or automatic force control can adapt gripping force to delicate profiles. This reduces localized crushing, flattening, and loss of roundness while maintaining enough grip to prevent slipping.
- Continuous Tube Support: Rollers, guides, and follower supports carry the tube during loading, feeding, and rotation. Properly positioned supports shorten unsupported spans, reducing sagging and vibration in long or slender tubes. Support height must be aligned correctly to avoid introducing a bend.
- Synchronized Motion: Coordinated chuck rotation and lengthwise feeding keep the tube moving smoothly. Acceleration and rotational speed suited to the tube’s stiffness help limit whipping and twisting. Stable motion also helps maintain a consistent nozzle gap and cutting conditions around the profile.
- Planned Cutting Sequences: CAD/CAM programming can distribute cuts across different areas to prevent concentrated heating and preserve stiffness while machining weak sections. Where appropriate, internal features are completed before final separation. The sequence should avoid leaving fragile, heavily perforated sections unsupported during later cuts.
- Supported Part Release: Suitable unloading supports and controlled handling prevent finished parts from bending under their own weight or being damaged by dropping. Supporting the component during its final separating cut is particularly important for long parts and tubes weakened by numerous openings.